Guide
Inkjet ink and substrate guide
How the packaging material, surface finish and production environment affect inkjet coder selection and ink choice.
Application fit
Start with the surface you need to print onto
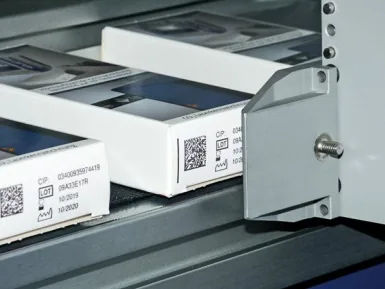
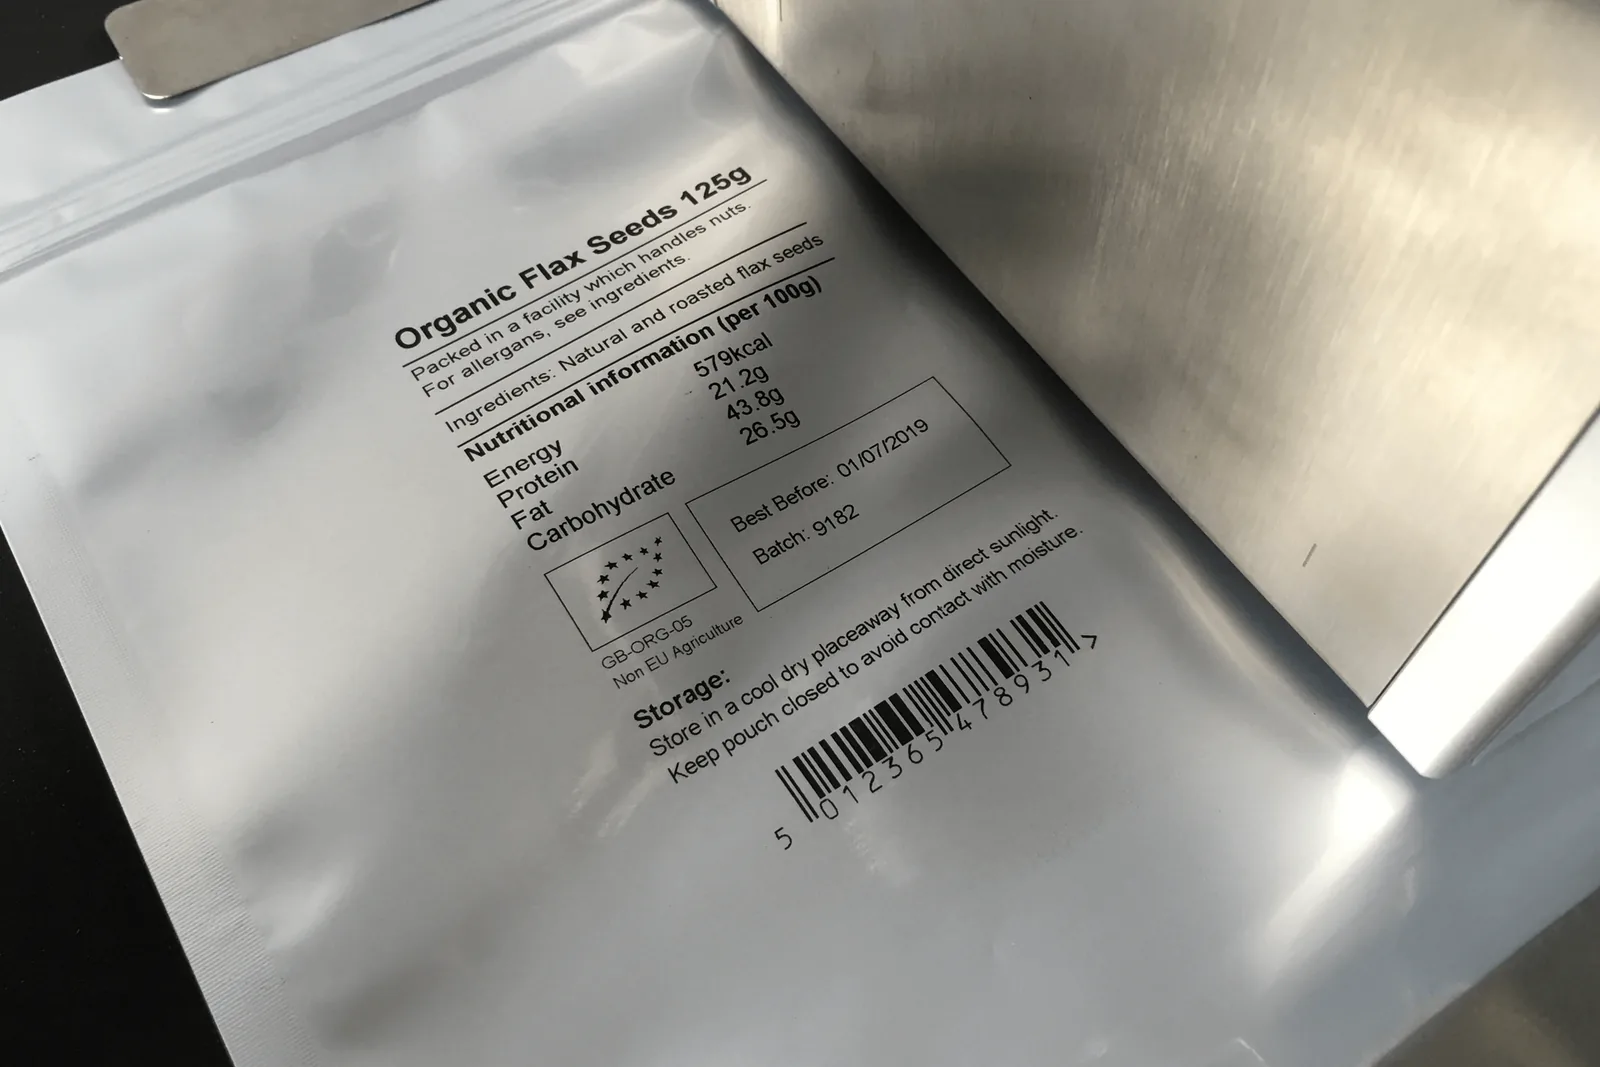
A code that looks clear on a carton may not work on a wet bottle, glossy pouch or curved plastic tub. The substrate, coating, surface energy, temperature and handling after print all affect ink adhesion and dry time.
- Test actual production packaging, not only supplier samples
- Check adhesion after handling, packing, chilling or palletising
- Confirm whether the surface is porous, coated, glossy, wet, dusty or oily
- Match the coder technology to the print height, resolution and line speed
| Porous surfaces | Uncoated cartons, corrugate and some paper labels can often accept fast-drying high-resolution print |
|---|---|
| Non-porous surfaces | Plastic, glass, metal and films usually need matched ink and dry-time testing |
| Flexible packs | Pouches, bags and sleeves need checks for movement, gloss, heat seal area and code position |
| Related options | Code quality guide, pouch coding and thermal inkjet printers |
Specification notes
Practical checks before selecting a machine
Use these checks before you buy, quote or install a coder. They help reduce print defects, missed codes and unreliable date or batch marking once the line is running.
Have a sample, photo or line video?
Send detailsSend it with your enquiry so the coder type, bracket position, print head access and ink choice can be reviewed properly.
Related options
Helpful inkjet coding options
Compare related coder types, applications and specification guidance.
Pouch and film coding
Date, batch and traceability printing on pouches, bags, labels, sleeves and flexible packs.
View details →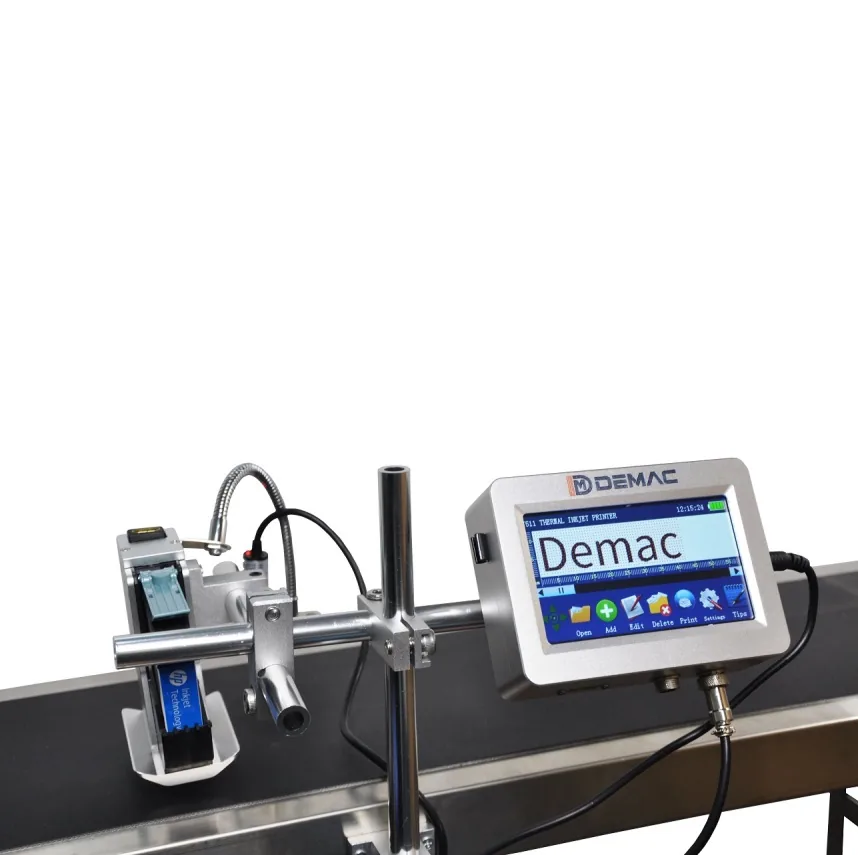
Thermal inkjet printers
High-resolution TIJ print for cartons, labels, sleeves, QR codes and barcodes.
View details →Next step
Get a practical coding recommendation
Send pack photos, code artwork, material, speed, code position and available line space. Lancing can then advise on the most suitable inkjet coding route.
Need to print date, batch, lot or QR codes?
Tell us what you need to code and where the coder has to fit on the line.
Compatibility testing
Approve ink on the real production surface
Material names such as PET, HDPE, glass or cardboard do not fully describe a printable surface. Supplier, coating, colour, recycled content, treatment and contamination can all change adhesion and contrast.
1
Collect representative samples
Include every approved supplier, colour, size, coating and the oldest or most difficult normal stock. Condition samples as they are at the coding point.
2
Define the code and settings
Use the actual message, print height, resolution, speed and throw distance. Record printer, ink or cartridge and all relevant settings.
3
Measure dry time
Check at the first contact point on the line and after the normal interval before packing. Note temperature, humidity and surface condition.
4
Apply the expected handling test
Use a controlled rub, wipe, tape, scratch, water, oil or chemical exposure only where it represents the real requirement.
5
Inspect legibility and codes
Check visual quality and, where relevant, scan or verify the machine-readable symbol on the final pack.
6
Record and control the approval
Retain samples, photographs, settings, consumable references and the acceptance decision. Re-test after material or process changes.
| Surface issue | Possible effect | What to investigate |
|---|---|---|
| Condensation | Beading, weak adhesion or delayed drying | Coding point, surface drying, ink chemistry and handling time |
| Oil or mould release | Code separates from the substrate | Normal contamination level, cleaning feasibility and specialist ink |
| Coating or varnish | Poor wetting or slow drying | Exact coating reference and alternative print zone |
| Rough or porous board | Ink spread and broken edges | Ink viscosity, resolution, printhead type and board grade |
| Dark or clear pack | Low visual contrast | Contrasting ink, background panel, label or different code position |
| Flexible or moving surface | Distorted characters or changing print gap | Support, guides, coding before forming or alternative technology |
Running-cost data belongs in the trial
Record nozzle purging, cartridge wiping, make-up use, rejected starts and cleaning time. A consumable that prints well but requires frequent intervention may not be the lowest-cost production choice. Use the same message coverage and operating pattern when comparing options.
Related substrate-specific applications
Send samples in their normal production condition and state the required resistance test.
Arrange a substrate reviewRepeatable approval
Turn ink adhesion and durability into controlled acceptance criteria
“Permanent” or “quick drying” is not a complete test requirement. Approval should define the substrate, conditioning, print settings, elapsed time, exposure, inspection method and pass rule so the result can be repeated after supply.
| Test stage | Method to define before testing | Information to record |
|---|---|---|
| Sample identity | Approved supplier, material grade, coating, colour, recycled content, manufacture date and normal surface condition. | Sample reference, batch or lot, photographs and any cleaning or conditioning applied. |
| Print setup | Printer, printhead, ink or cartridge, message, resolution, speed, orientation and print distance. | All settings, consumable batch, environment and operator so the result can be reproduced. |
| Dry-time check | First downstream contact and the practical intervals at which the pack is touched, guided or packed. | Elapsed time, visible transfer, smearing, handling point and surface temperature or moisture where relevant. |
| Rub or abrasion | Contact material, force or controlled method, number of passes and direction representing real handling. | Before-and-after photographs, legibility and the agreed pass or fail decision. |
| Water, oil or chemical exposure | Actual production substance, concentration, contact method, duration and recovery time. | Ink change, loss of contrast, transfer, substrate damage and safety controls used during the test. |
| Machine-readable code | Symbol, reader or verifier, lighting, orientation, sampling plan and minimum result where required. | Individual results, final-pack image, failed examples and any relationship to surface variation. |
| Ageing and storage | Expected temperature, humidity, sunlight, refrigeration, stacking and time before assessment. | Storage conditions, dates, code condition and whether the pack or coating changed. |
Control consumable identity
Retain the full ink, make-up fluid or cartridge reference, colour, batch where available, expiry or shelf-life information and storage requirements. Similar names or colours do not prove the chemistry is interchangeable.
Use current safety information
Obtain the applicable safety data and follow the supplier's handling, ventilation, storage, spill and disposal requirements. Site risk assessment remains separate from proving print quality.
Approve the finished process
Test after the pack has passed through filling, cooling, sealing, labelling, case packing and other relevant stages. A clean empty sample may not represent the surface that reaches the production coding point.
Define when approval must be repeated
- New pack, resin, board, film, coating, colour or material supplier.
- New ink, fluid or cartridge reference, colour or formulation.
- Changed print position, speed, resolution, print distance or message coverage.
- Changed filling temperature, cleaning chemical, refrigeration or handling process.
- Changed barcode or 2D size, data density, reader or verification requirement.
- Recurring defects or field evidence that the approved condition is no longer representative.
Separate print quality from running cost
First prove the code against the required handling and inspection criteria. Then compare accepted codes per consumable, purging or wiping, make-up use, cleaning time, rejects and part-used consumable losses under the same operating pattern.
Continue with CIJ fluid planning, TIJ cartridge evaluation, code-quality checks and inspection and reject control.
Send production-grade samples and the resistance requirement.
Lancing can structure the coding trial around the real surface and downstream handling.